Why the first 10 minutes matter more than people think
In many CNC shops, the delay starts before the spindle turns. The operator is hunting for clamping notes, the programmer is answering questions, and somebody is still checking which tool was last used on the machine. A proper setup sheet cuts through that mess. It tells the team what to load, what to measure and what to verify before the job goes live.
For South African shops that run mixed batches, this matters even more. If you are doing a small aluminium run in Centurion in the morning and a steel repair job in Johannesburg after lunch, you cannot afford vague instructions. A useful setup sheet reduces guesswork, keeps the job moving during load-shedding windows, and helps a standby operator pick up where the previous shift left off.
The details a good setup sheet should never leave out
Some sheets are little more than a job number and a part name. That is not enough. The best setup sheets carry the practical details that stop rework, tool breakage and wasted material. They should be short enough to use on the shop floor, but complete enough to answer the questions that always come up at the machine.
- Part name, drawing revision and job number
- Machine type, controller and programme file name
- Material grade, thickness or stock size
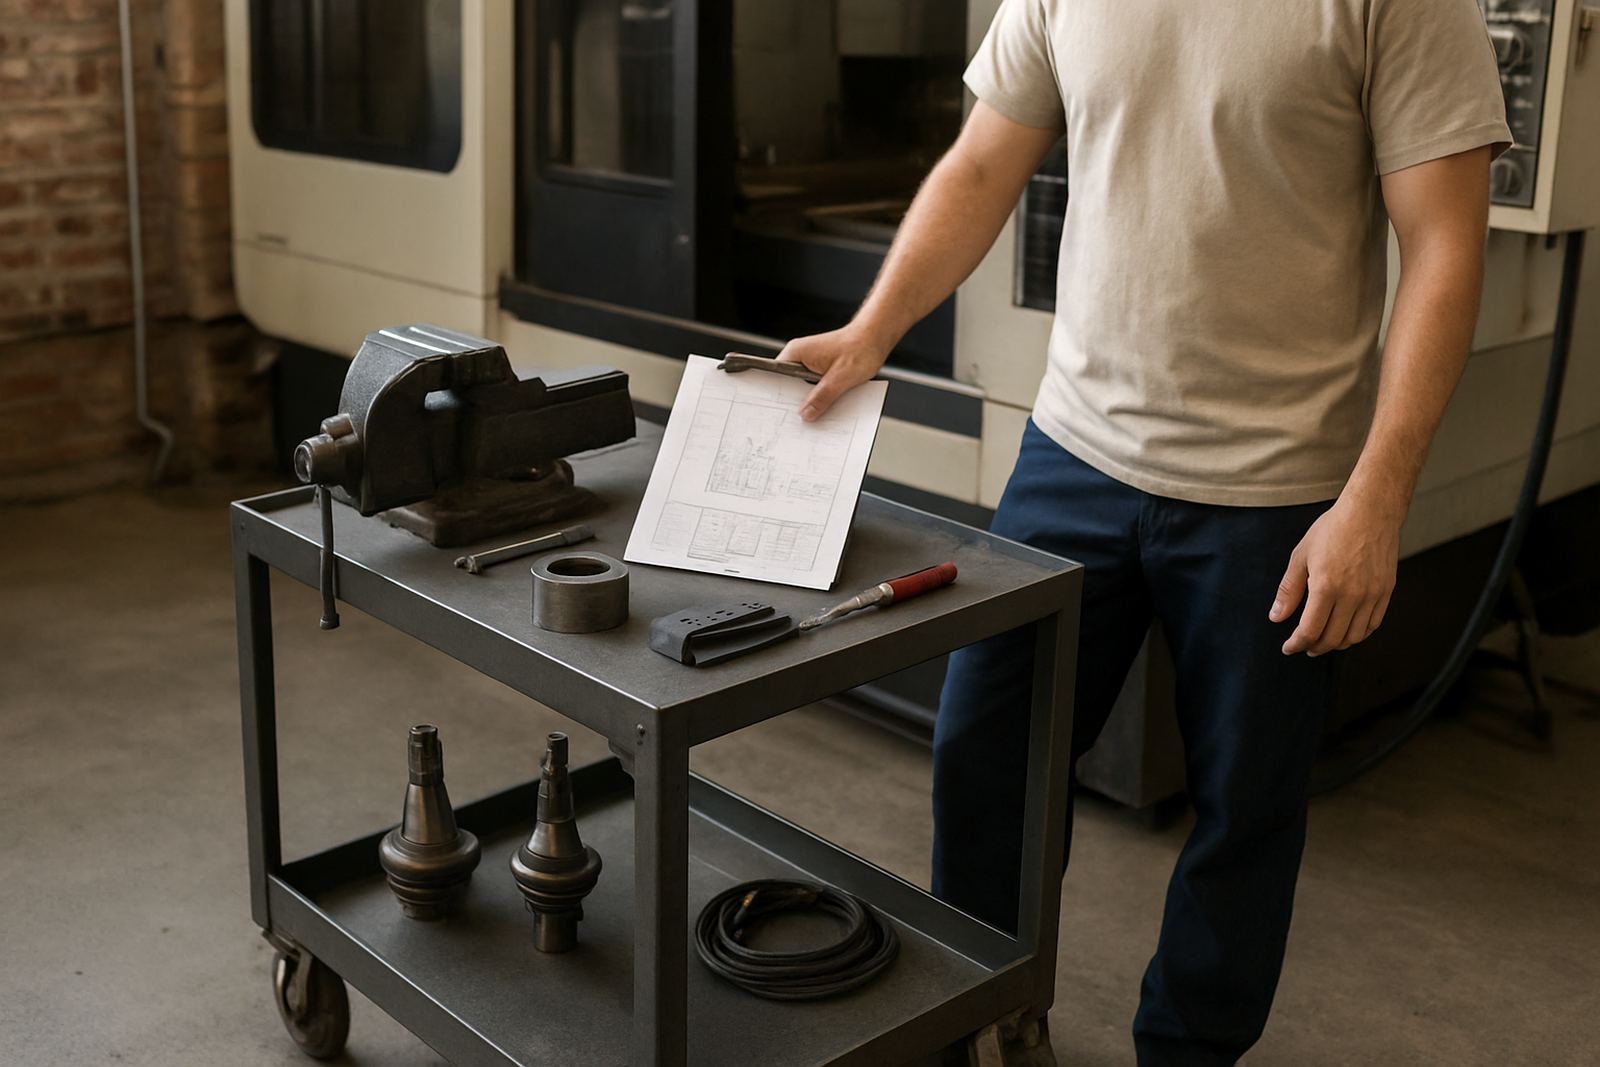
- Vice, fixture or table layout with zero point location
- Tool list with lengths, diameters and offsets
- Safe start position, feed and speed notes
- Inspection points and critical dimensions
- Any special warnings for coolant, tabs or soft jaws
If a shop in Durban is working near the coast, the sheet should also note any handling or storage steps for material that picks up moisture. In Vereeniging, where some workshops run with older machines and mixed tooling, it helps to note exactly which gauges or holders must be checked before clamping. Small notes save time when the team is busy and the pressure is on.
How setup sheets cut changeover time on the shop floor
The real value of a setup sheet is not paperwork, it is speed. When the operator can see the clamping method, tool order and first-off checks at a glance, the machine can be prepared without stopping to ask three different people for the same answer. That means shorter changeovers and fewer interruptions when the phone rings or a job needs to restart after a power cut.
Well written sheets also reduce the risk of using the wrong offsets or loading the wrong programme version. In a busy milling department, that can be the difference between a clean first article and a scrap part. On a turning job, it can stop a bad tool path from running into the chuck jaws. That is money saved, not just time.
What should be written for routing, milling, turning and plasma
Every process needs a slightly different setup sheet. A routing job needs board size, hold-down method and where the cutter exits the material. Milling needs datum position, vice setup and tool length checks. Turning needs jaw height, bar stock length and boring tool clearance. Plasma work needs torch height, sheet flattening and safe lead-in notes.
- Routing: spoilboard condition, vacuum zones, tab positions and dust extraction checks
- Milling: workholding orientation, cutter stick-out and probing sequence
- Turning: chuck grip length, tailstock use and part-off clearance
- Plasma: sheet flatness, earth clamp position and cut order to reduce distortion
When these notes are consistent, the operator does not have to interpret the programmer’s thinking. The instructions are there, plain and simple. That is especially useful where a second shift or relief operator steps in after lunch or after a municipal outage.
Local example from a Centurion job sheet
One Centurion shop running both routing and milling jobs had a recurring problem with slow starts on Monday mornings. The machine was ready, but the team still spent 15 to 20 minutes checking tool lists, clamp positions and which file matched the latest drawing. The setter had one version, the programmer had another and the operator was relying on memory.
After tightening the setup sheet format, each job now opens with the same core details: file name, revision, machine, tool list, clamping sketch and first-off check. The result was faster changeovers and fewer calls back to the office. Nothing fancy, just clearer instructions. They also added a short note for jobs likely to run during load-shedding so the restart sequence was ready if power dropped mid-cycle.
Make the sheet part of the workflow, not a last-minute extra
A setup sheet works best when it is built into the job release process. The programmer should not be scribbling notes at the machine after the file is already loaded. The information must be ready before the job reaches the floor, with the same structure every time. That way, training new operators becomes easier and support calls become more specific.
If your shop is still relying on memory, old notes or a photo on a phone, the process is costing you more than you think. A better sheet gives the team one source of truth for each job and makes the handover cleaner from office to machine. For shops across Pretoria, Johannesburg, Cape Town and Durban, that is a practical improvement you can feel in the first week.
At CNC Software, we help CNC shops build better post-process output, cleaner job setup and clearer handover habits. That includes training, workflow audits and first job support when you need a practical hand on site. If your current sheets are missing key details, we can help you tighten the format so the machine is ready sooner and the first part comes out right.